PRECISION FEATURE
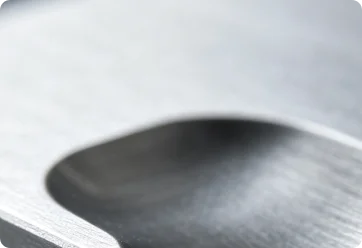
R0.11mm
Sharp internal corners with standard 0.20mm wire, a geometry CNC milling can't replicate.
Partner with Unionfab, a China-based wire EDM manufacturer integrating in-house wire EDM capabilities with a network of 300+ vetted suppliers, to produce precision profiles and narrow slots in tool steel, carbide, and titanium, with sharp corners and tight dimensional control.

STEP | STP | IGS | DWG | DXF | PDF Files and More
Get Wire EDM Machining Quote No MOQ • ISO 27001 Certified • Free DFM Analysis

PRECISION FEATURE
Sharp internal corners with standard 0.20mm wire, a geometry CNC milling can't replicate.
MATERIAL CAPABILITY
Machines hardened tool steel and titanium with ease, where conventional cutting tools struggle.
MANUFACTURING SCALE
400+ advanced CNC machining centers (Mazak, DMG MORI, Makino etc.) in 4 in-house facilities.
CERTIFIED
ISO 9001, 14001, 13485 & IATF 16949 certified with NDA-secured manufacturing workflows.
Wire EDM (Wire Electrical Discharge Machining) is a highly precise, non-contact process that uses a thin, continuously moving wire to cut electrically conductive materials. Instead of applying physical tool pressure, it follows a CNC-programmed path and removes material through controlled electrical discharges between the wire and the workpiece, leaving burr-free edges with minimal mechanical stress on the material.
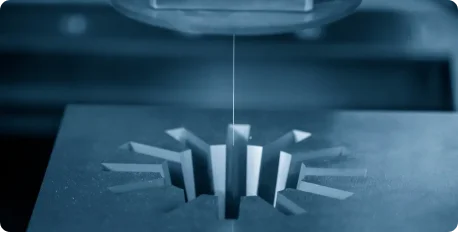
Wire EDM is best suited for electrically conductive parts that demand tight tolerances, ultra-fine internal geometry, or hardness levels beyond the reach of conventional cutting tools. If your part fits any profile below, Wire EDM is ideal for your project.
Ideal for parts requiring tolerances as tight as ±0.0002", near-sharp internal corners, narrow slots, or complex profiles that conventional tooling cannot reach.
Cut without mechanical distortion, ideal for pre-hardened tool steel, carbide, titanium, and high-temp alloys.
Excellent for fragile or thin-walled components where zero mechanical cutting force is required to eliminate deflection, warping, or material damage.
Delivers clean, burr-free edges straight off the machine, thus eliminating costly secondary deburring for high-precision medical, aerospace, and electronic parts.
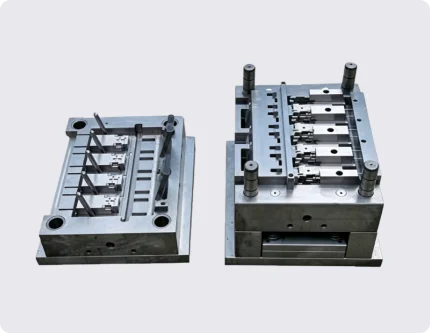
Tailored for mold inserts, punches, extrusion dies, and cavity components requiring precise 2D/2.5D contours directly cut into hardened tool steels.
Ideal for intricate contours, taper angles, or rapid prototypes where fast setup, zero tooling cost, and geometric flexibility outweigh cutting speed.
We machine a broad range of electrically conductive metals to meet the performance requirements of your application.
Tool steel offers excellent hardness and wear resistance after heat treatment, making it a core material for EDM. Because EDM removes material through spark erosion rather than cutting, hardness has little effect on process speed, allowing precise features to be formed even after hardening.
Ideal for: Mold cavities, punches and dies, stamping tools, precision fixtures
Available Grades: A2, D2, O1, S7, H13, P20
We offer a range of post-processing options to meet your part's surface, tolerance, and functional requirements.
Skim cutting uses one or more finishing passes with finer discharge parameters to improve surface finish and dimensional accuracy after the initial EDM cut. It is especially common in wire EDM, and similar finishing passes may also be used in sinker EDM applications where tighter surface requirements are needed.
Best For: Precision mold components, sealing surfaces, parts requiring tighter tolerances
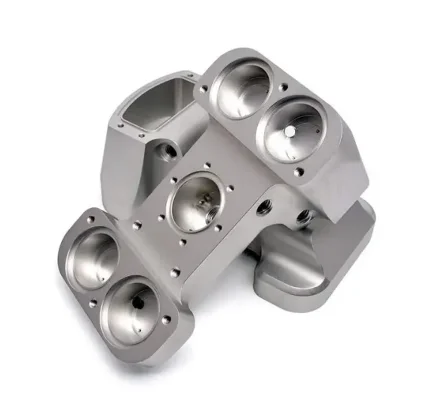
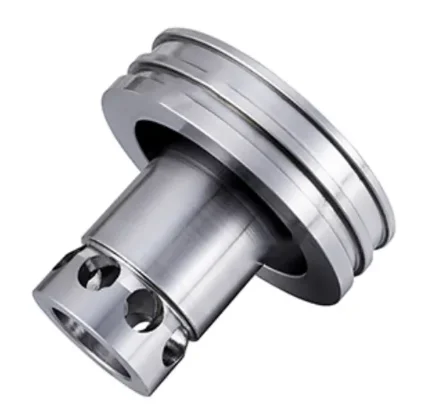
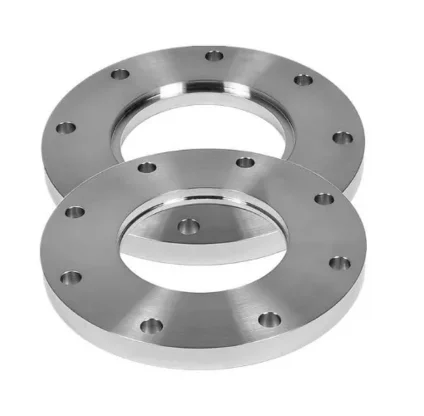
| Parameter | Standard Capacity | Large-Bed Capacity |
|---|---|---|
| Max. Part Length (L) | 500 mm (19.7") | 1,000 mm (39.4") |
| Max. Part Width (W) | 350 mm (13.8") | 800 mm (31.5") |
| Max. Part Height (H) | 250 mm (9.8") | 400 mm (15.7") |
| Min. Part Thickness | 0.5 mm (0.020") | 0.5 mm (0.020") |
*Note: Max. Part Length/Width refer to maximum workpiece dimensions, not machine axis travel; actual capacity depends on table size, clamping method, and part geometry. Parts thinner than 1.0 mm require dedicated fixturing to reduce vibration and distortion.

While our instant quoting platform uses your 3D CAD files for geometric pricing, any custom dimensions, GD&T callouts, specific fits, or tight surface finishes MUST be explicitly detailed in an accompanying 2D PDF drawing.
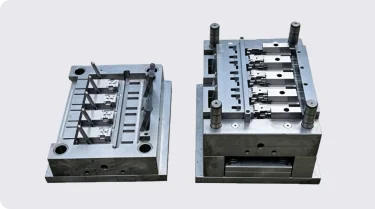
Wire EDM is a core process for producing stamping dies, punches, and mold inserts, cutting hardened tool steel and carbide with tight internal corner radii and narrow slot widths that milling or grinding cannot achieve. Taper cutting capability also enables precise draft angles on punch profiles and die clearances in a single setup.
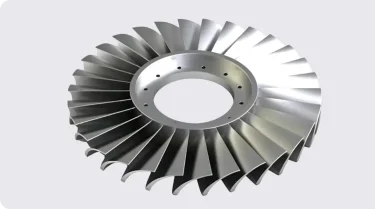
Wire EDM machines heat-resistant superalloys and titanium components used in turbine and structural assemblies, cutting complex through-profiles with tight positional accuracy. Because it's a non-contact process, it avoids the mechanical stress and tool wear that conventional cutting struggles with on these hard-to-machine materials.
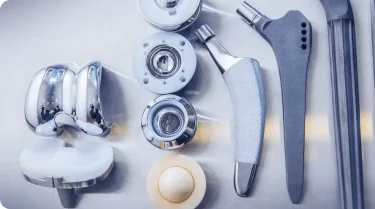
Wire EDM delivers the micro-feature precision required for surgical instruments and implant components, cutting narrow slots, fine internal contours, and thin-wall profiles to tight tolerances. Its clean-cut edges and repeatable accuracy support the surface quality standards required in medical manufacturing.
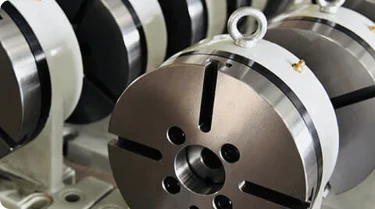
Wire EDM produces hardened, non-standard components such as gears, cams, and precision guide features, where complex 2D profiles and tight dimensional control are critical. It's especially suited for low-volume or one-off precision parts that would require expensive custom tooling with conventional machining.
| Factor | Wire EDM | CNC Milling | Laser Cutting |
|---|---|---|---|
| Material compatibility | Conductive metals only | Almost all metals, plastics, composites | Metals and some plastics |
| Hardness handling | Tolerance unaffected by hardness | Tool wear increases with hardness | Moderately affected |
| Max part thickness | Excellent: 100-400+ mm with consistent verticality | Limited by tool overhang length | Best for 0.5-20 mm |
| Geometry capability | 2D / 2.5D profiles, including taper cuts | Full 3D: pockets, curves, blind holes | 2D planar only |
| Cutting forces | None: fully non-contact | High mechanical force | Very low, non-contact |
| Edge quality | Burr-free, no secondary finishing | Burrs common, needs deburring | Minimal burrs, possible heat-affected zone |
| Achievable tolerance | Down to ±0.0008" | Typically ±0.001"-0.005" | Typically ±0.002"-0.004" |
| Internal corners | Near-sharp (wire-diameter limited) | Limited by tool diameter | Limited by kerf width |
| Cutting speed | Slower: spark erosion, not shearing | Moderate to fast | Very fast on thin sheet |
| Best for | Hardened tooling, precision slots, tight tolerances | Structural parts, complex 3D shapes | Sheet metal, enclosures, fast turnaround |
We adhere to a strict multi-stage inspection protocol to ensure every part meets your exact specifications.
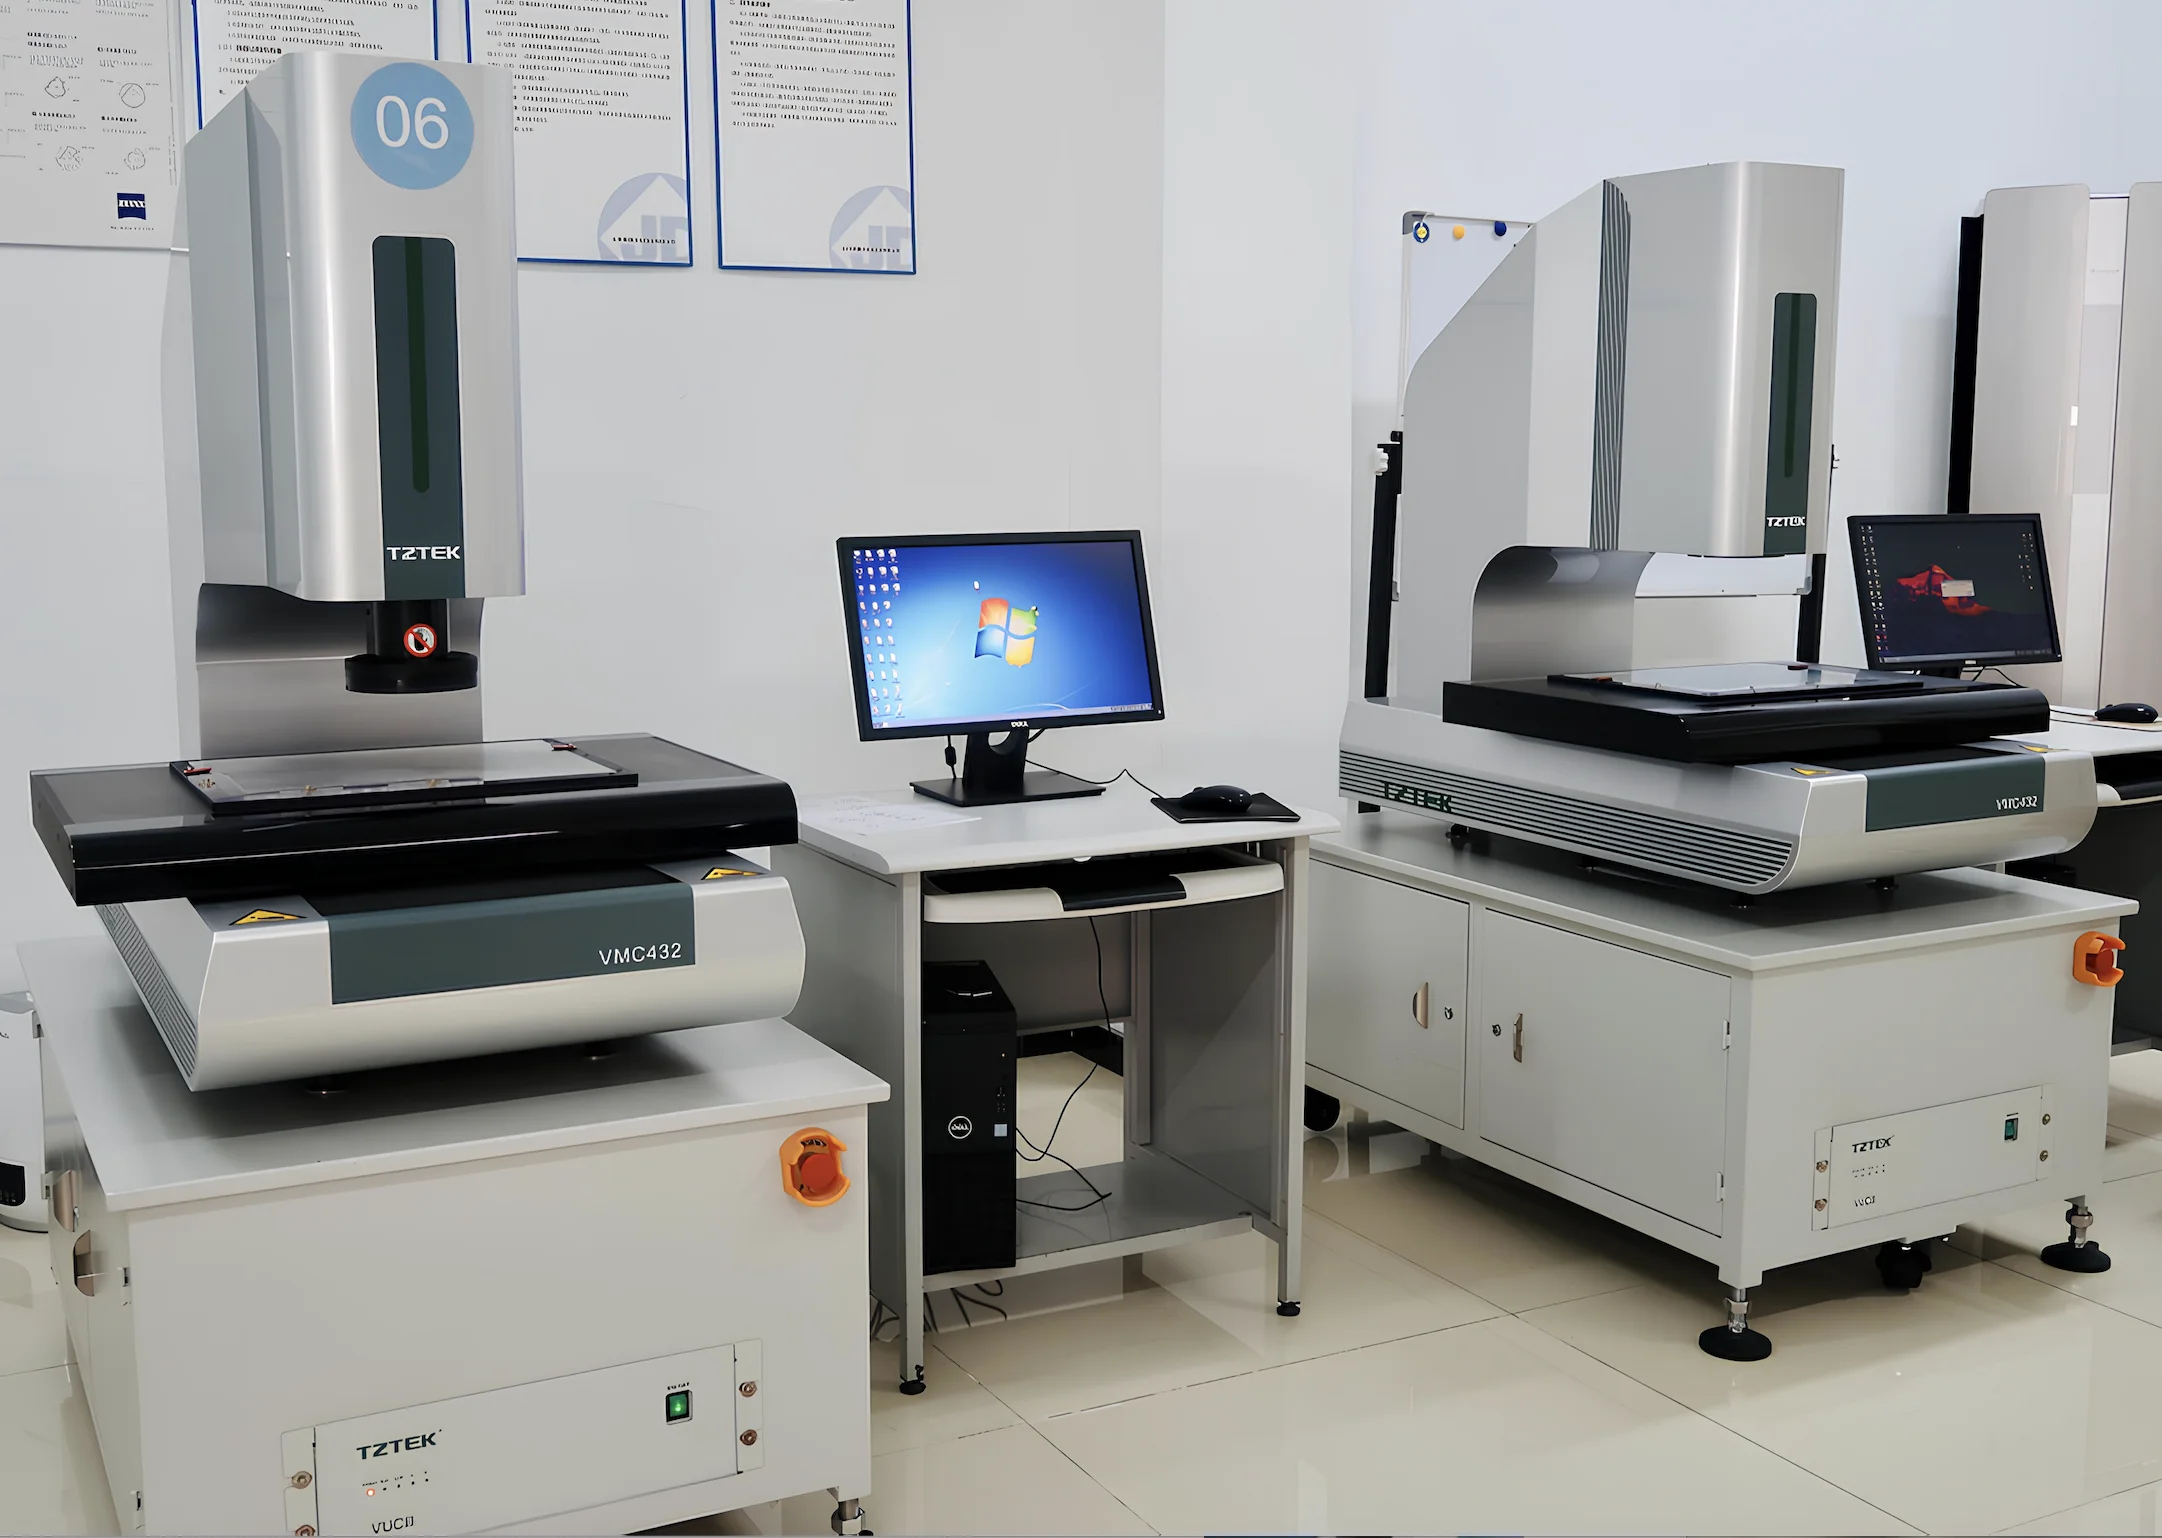
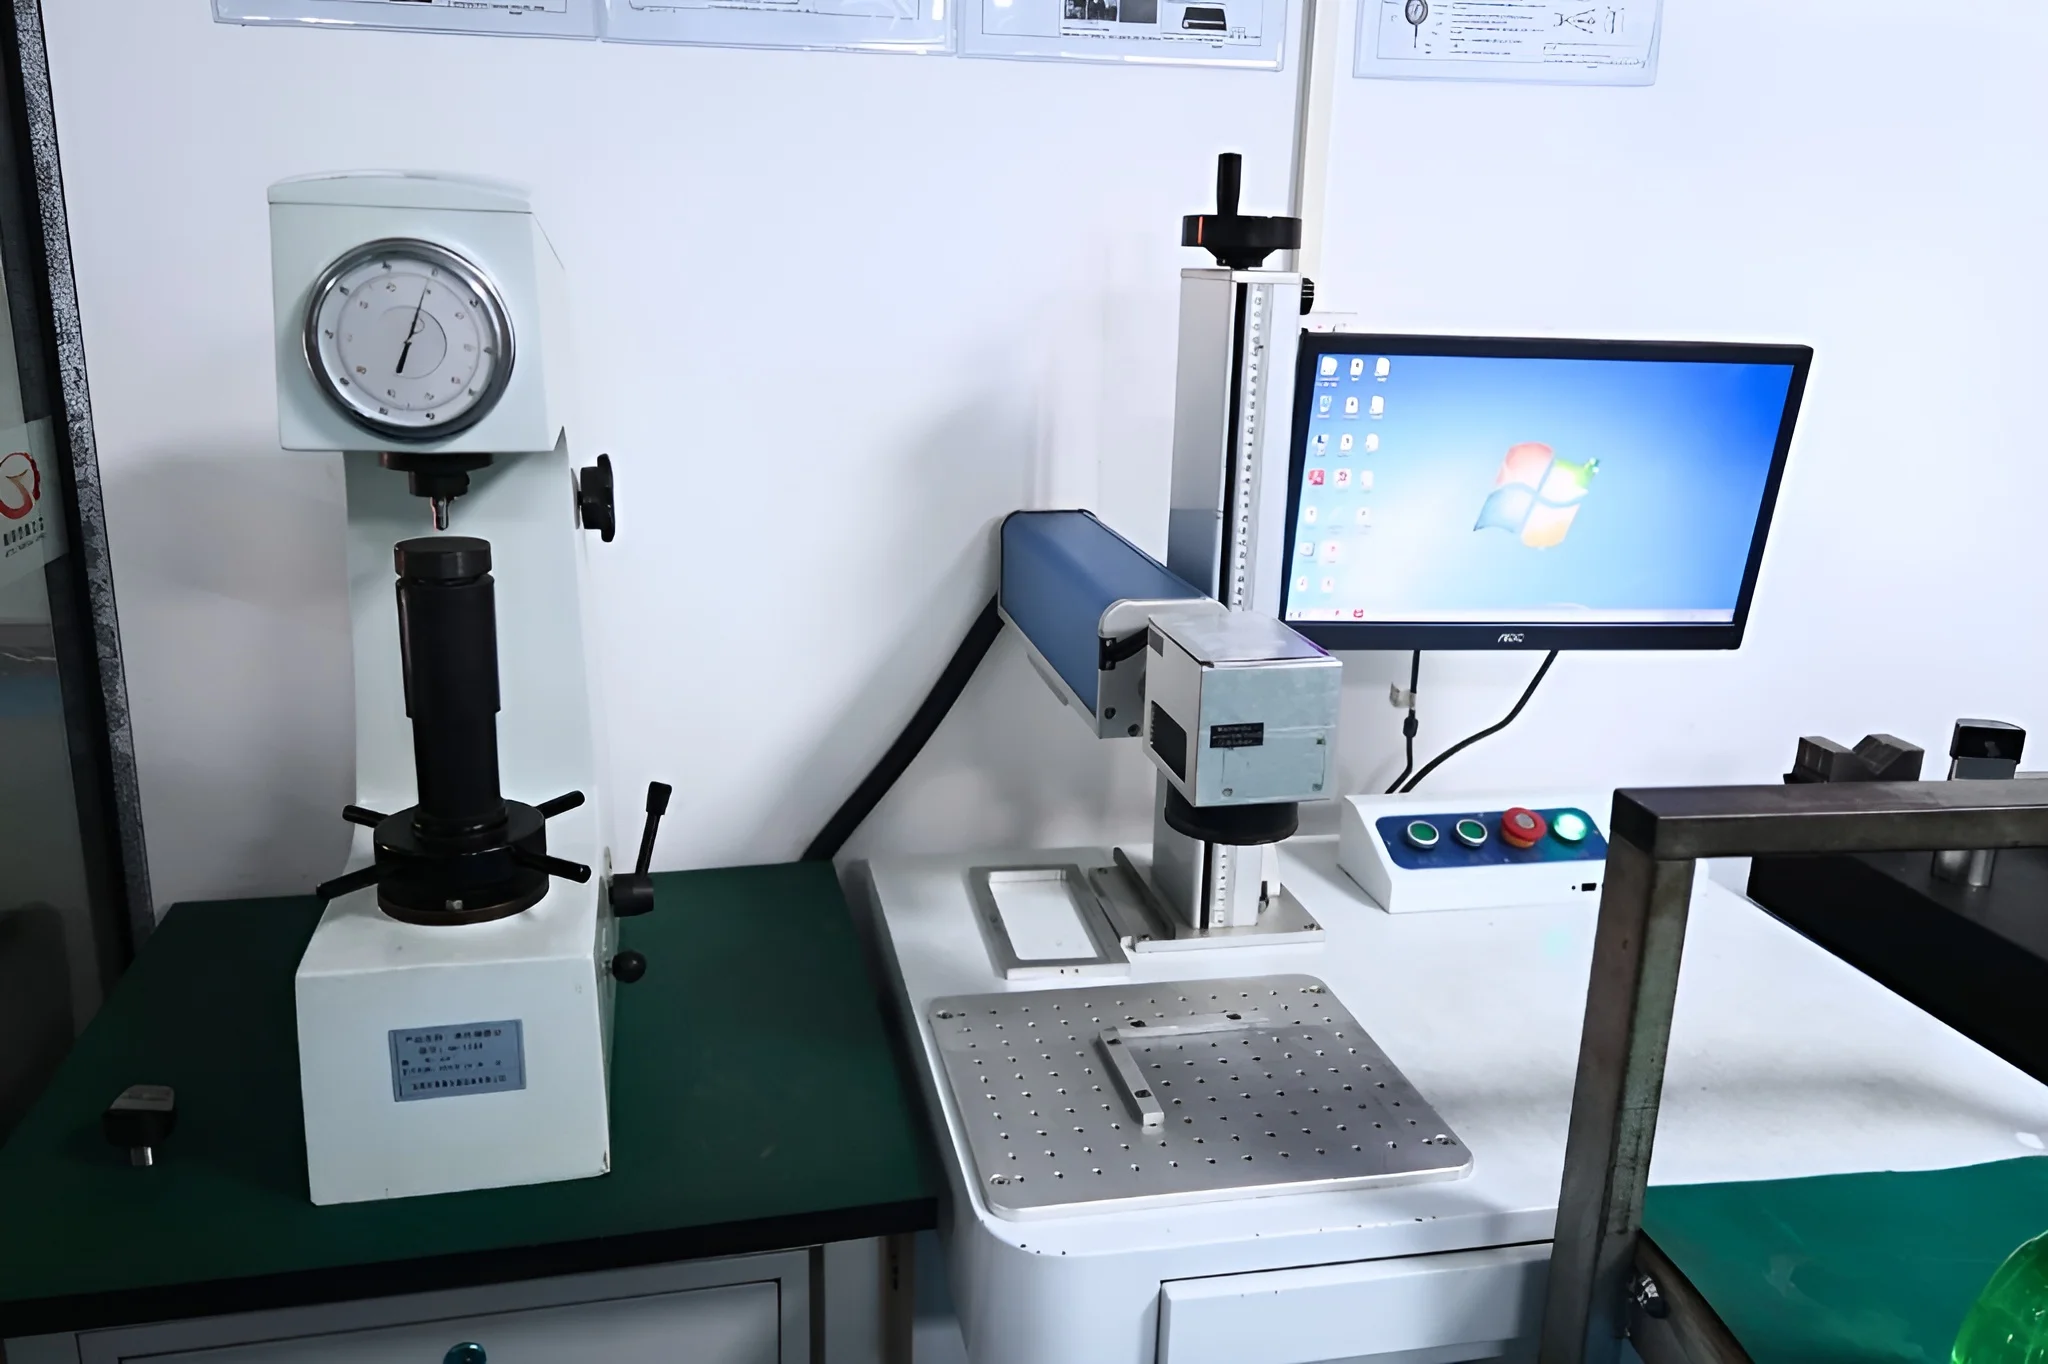
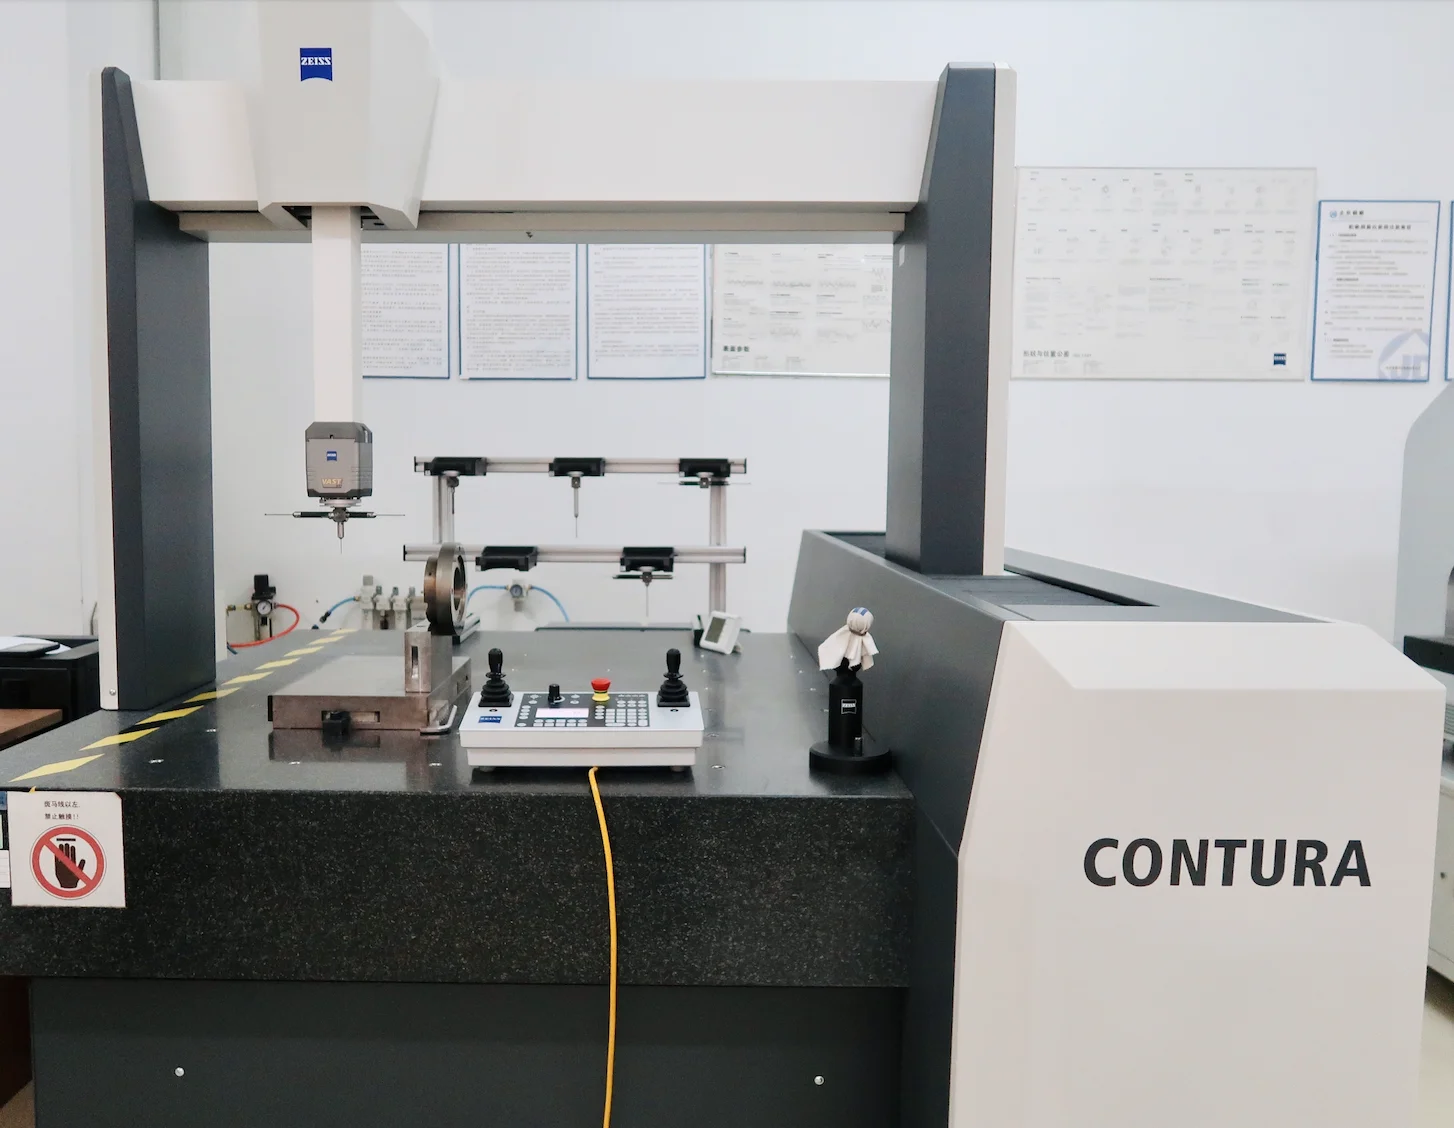
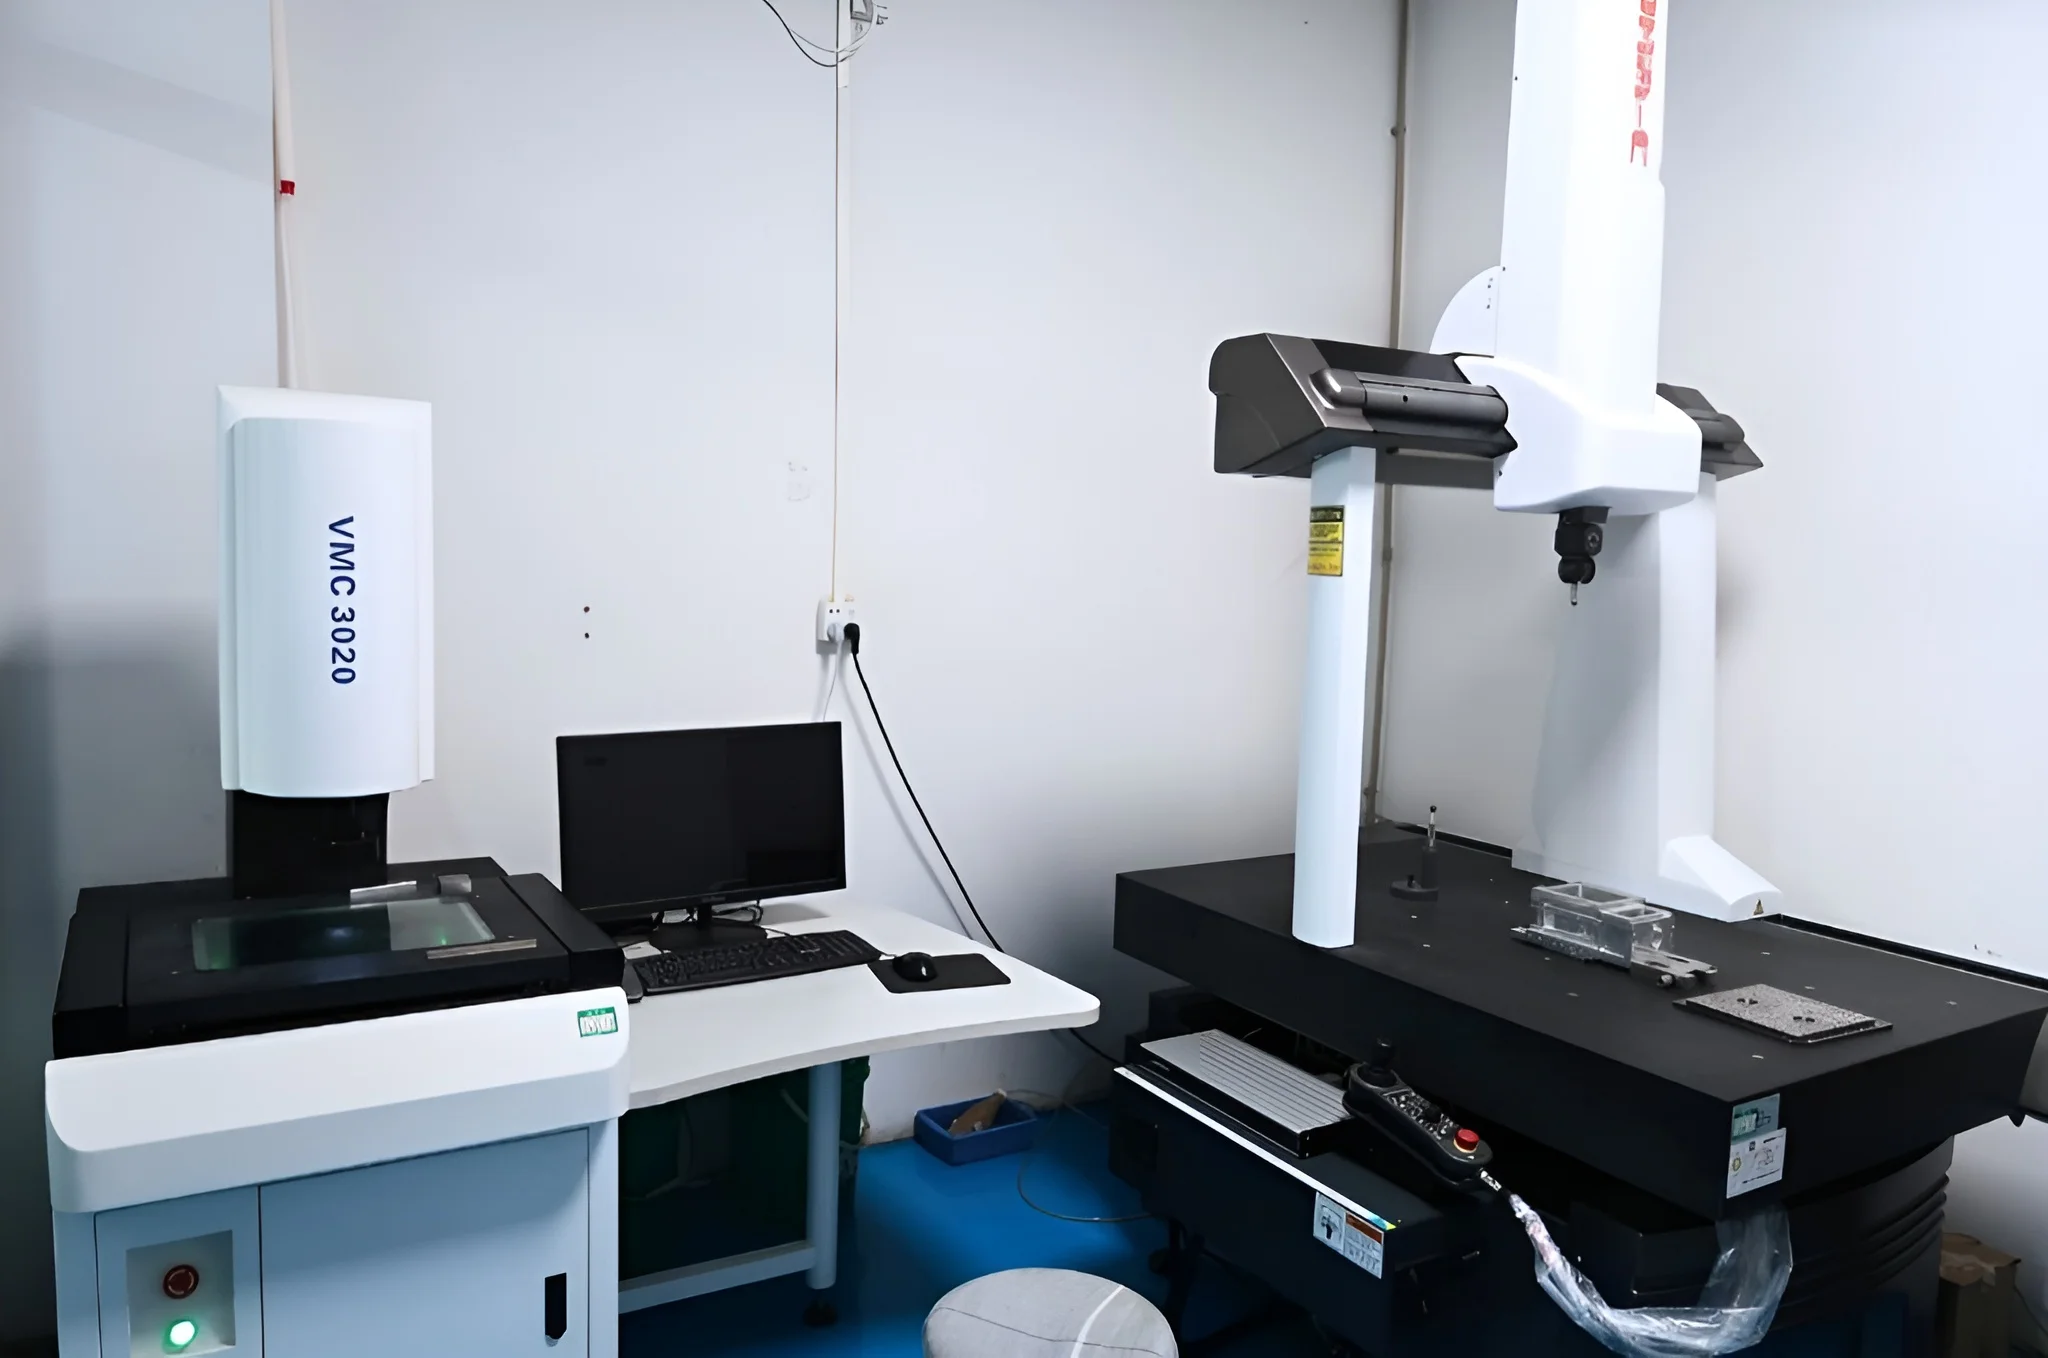
Every order includes a First Article Inspection report (upon request).
We utilize state-of-the-art CMM (Coordinate Measuring Machines), profilometers for surface roughness, and calibrated hand tools.
All material certifications and heat treatment reports are archived and available for audit.
Our quality systems are aligned with international ISO 9001 standards, covering dimensional, geometric (GD&T), and material requirements.
For more details on our quality standards, check out our Inspection Checklist (including both standard and premium options).
We accept both 3D models and 2D drawings. For instant geometry analysis and baseline pricing, please upload your 3D CAD files in STEP, STP, or IGS formats. If your part requires specific tight tolerances, GD&T callouts, or threaded holes, a supplementary 2D drawing in PDF, DWG, or DXF format is required.
We have no strict Minimum Order Quantity (MOQ = 1). Whether you need a single rapid prototype for design validation or a low-volume production run of thousands of parts, our flexible manufacturing network is built to scale with your project efficiently and cost-effectively.
Our standard manufacturing lead time for most CNC projects is 5 business days. For exceptionally simple parts or urgent prototyping needs, we can expedite production and ship in as fast as 1 day. (Please note: Lead times may vary depending on part complexity, total quantity, and any secondary surface finishes required.)
100% Yes. We take intellectual property (IP) protection and data security incredibly seriously. We are proudly ISO 27001 Certified for information security management. Your files are encrypted and shared exclusively with essential engineering staff. We are also fully prepared to sign your Non-Disclosure Agreement (NDA) before you share any CAD files.
Absolutely. By default, every order includes a standard Dimensional Tolerance Report. For production volume orders, we supply comprehensive First Article Inspection (FAI) reports. If your critical components require ultra-precision metrology, full CMM (Coordinate Measuring Machine) inspection is available for an additional fee.
For a deep dive into our quality control processes, please read our guide on Unionfab QC & Inspection Capabilities.
Wire EDM Explained: Your Complete Guide to Precision Machining
Want to machine parts with extreme precision, no mechanical stress, and excellent surface finish? Wire EDM is your answer. In this guide, we’ll show you how it works, what it’s good for, and how to get the most out of it.
CNC Machining Price Guide: Breakdown & Price Comparison
Break down CNC machining prices, learn cost-saving strategies, and compare several major CNC service providers.
3D Printing vs. CNC Machining
Discover the key differences between 3D Printing and CNC Machining. Learn about their processes, materials, benefits, and best use cases in manufacturing.

Unionfab is China's Largest 3D Printing Manufacturing Company for Rapid Prototyping and On-Demand Production Parts.


