Learn how MJF 3D printing works, explore materials, costs, post-processing, and design tips, and compare MJF with other processes and service providers.
Introduction
When you need to produce functional plastic parts quickly, especially in complex geometries or low-volume production runs, the choice of 3D printing technology matters. FDM offers accessibility and flexibility, while SLS is well suited for strong, complex plastic parts. But what if you need fast production, fine feature definition, and the ability to produce multiple parts in a single build?
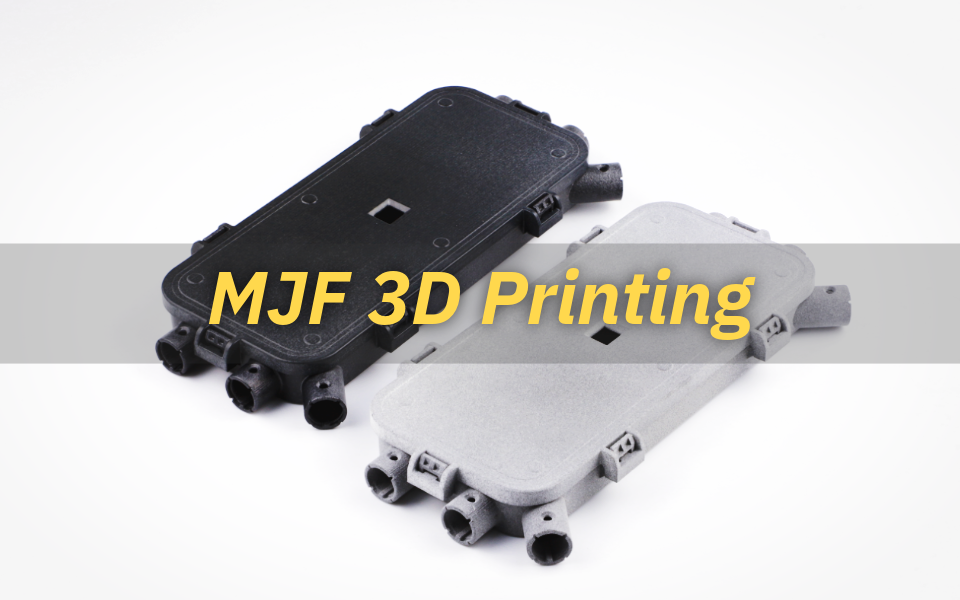
That's where Multi Jet Fusion (MJF) comes in. Developed by HP, MJF has become a widely used option for functional prototypes, customized components, and low-volume production, offering a balance of speed, part quality, and production efficiency.
In this guide, you'll learn how MJF 3D printing works, which materials it supports, how much it costs, and how to design parts for the process. We'll also compare MJF with SLS, SLA, and FDM to help you determine whether MJF is the right choice for your project.
What is MJF 3D Printing?
Multi Jet Fusion (MJF) is an industrial 3D printing technology developed by HP for producing functional plastic parts. It belongs to the powder bed fusion family and primarily uses thermoplastic powders such as PA12 and PA11 as its build materials.
In MJF 3D printing, a thin layer of polymer powder is spread across the build area. Printheads selectively apply specialized agents to define the areas that will become the part, and infrared energy then fuses the treated powder. This process is repeated layer by layer until the part is complete.
The result is a production-oriented 3D printing process capable of producing functional, detailed, and geometrically complex plastic parts.
How Does Multi Jet Fusion Work?
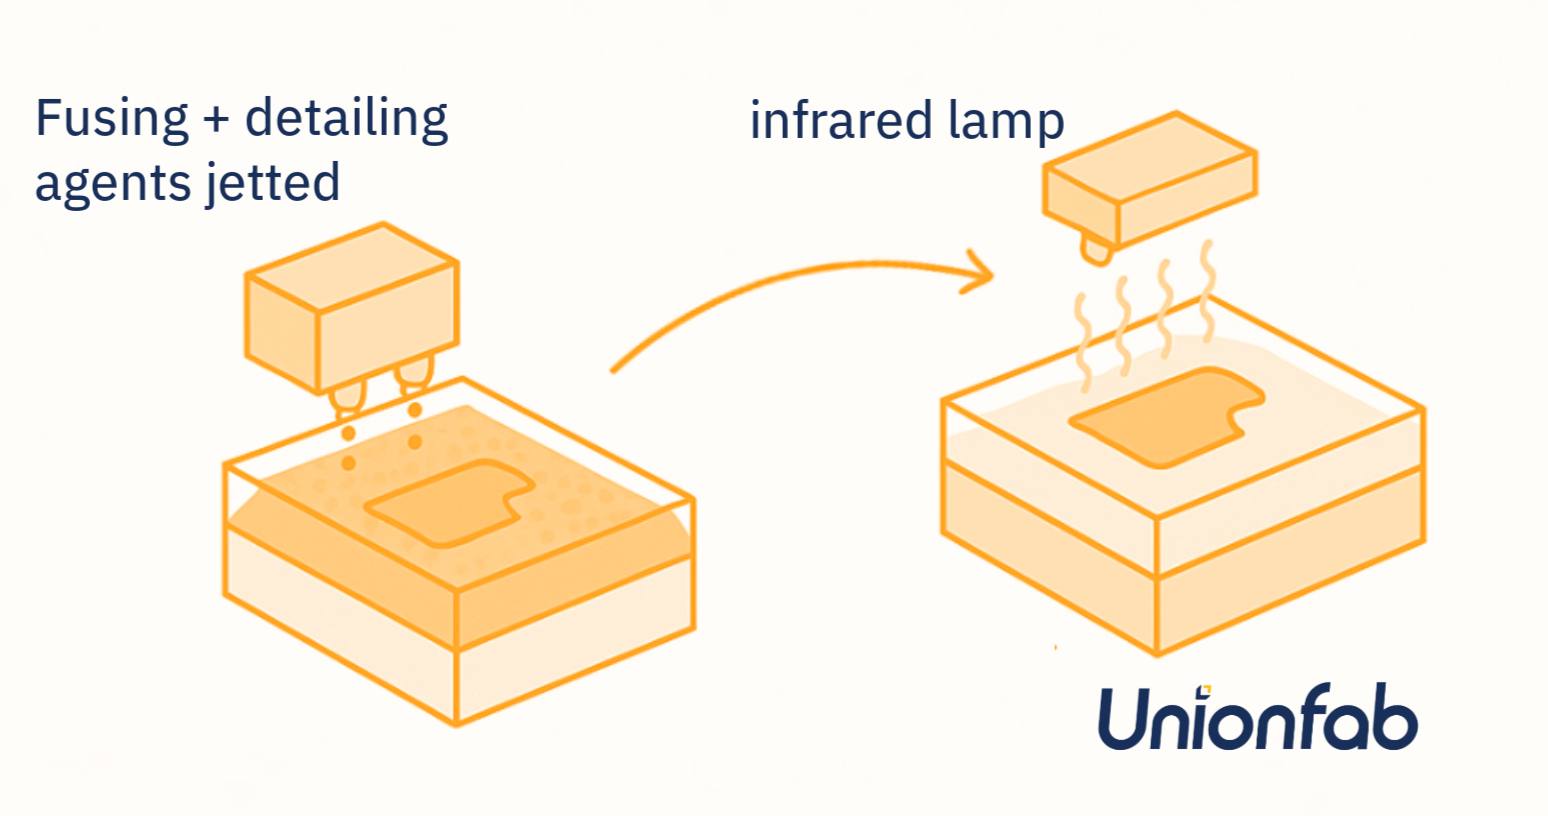
Instead of using lasers like SLS, MJF jets a fusing agent and detailing agent onto a powder bed, then fuses the material using infrared light. This speeds up the process and ensures consistent quality across builds.
Now let’s explore how this technology works under the hood:
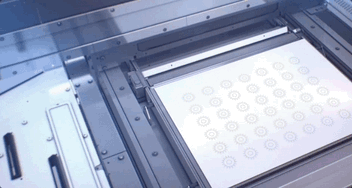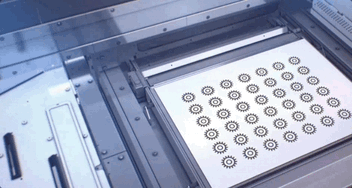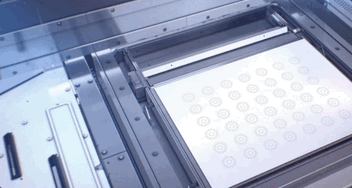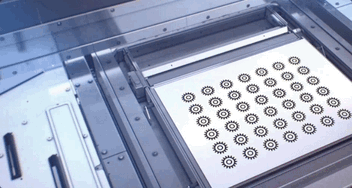
Source: MIT Fab Lab
MJF builds parts by selectively fusing polymer powder with a combination of jetting agents and infrared energy. The main steps are:
Powder deposition: A thin layer of polymer powder is spread evenly across the heated build platform.
Agent jetting: Inkjet printheads selectively deposit a carbon-based fusing agent on the areas that form the part, and a detailing (cooling) agent around boundaries to prevent thermal bleed.
Infrared heating: An infrared energy source passes over the powder bed. The fusing agent absorbs the energy and selectively melts the treated powder, while unprinted areas remain unfused.
Layer-by-layer building: The build platform moves down by one layer thickness (typically 80 microns), a new powder layer is deposited, and the agent-jetting and heating steps repeat.
Cooling and depowdering: After printing, the build unit cools in a controlled environment before parts are extracted, bead-blasted, and separated from unfused powder (which is reclaimed for future use).
Key Advantages of MJF 3D Printing
The following points summarize the main advantages of MJF 3D printing and their benefits for part production.
Fast Build Speeds: MJF applies fusing and detailing agents to each powder layer and uses infrared energy to fuse the selected areas. It is often efficient for producing multiple nested parts in one build.
No Traditional Supports: The surrounding powder supports the parts during printing, so separate support structures are usually unnecessary. This allows complex geometries and simplifies part removal.
Balanced Mechanical Properties: MJF parts generally offer relatively consistent mechanical properties across the X, Y, and Z directions, depending on the material and part design.
Powder Recovery: Unfused powder can be collected and reused. The recovery rate depends on the material, printer, and production setup.
Clear Feature Definition: Detailing agents help control heat around part edges, which can improve the definition of text, holes, corners, and other small features.
Efficient Batch Production: Multiple parts can be nested within the same build volume, making MJF suitable for customized parts, small production runs, and bridge production.
Flexible Post-Processing: MJF parts can be bead blasted, dyed, painted, coated, or vapor smoothed, depending on the desired appearance and performance.
Common Applications of MJF 3D Printing
Multi Jet Fusion (MJF) is widely recognized for its versatility, making it well suited to a wide range of industries and applications. With its speed, consistent quality, and functional mechanical properties, MJF is used to produce everything from functional prototypes to end-use parts.
Below are some common applications where MJF technology shines:
Industry | Applications | Parts Made by Unionfab | Key Benefits |
|---|---|---|---|
Automotive | Functional parts, in-car brackets | 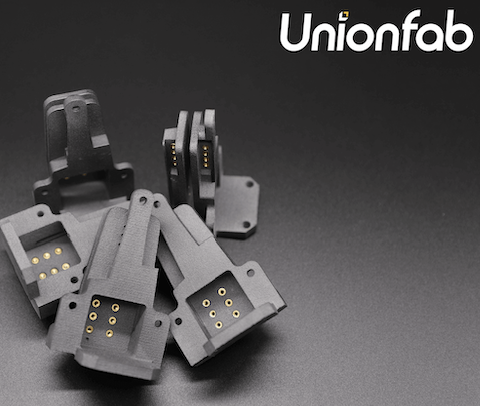 | Heat-resistant, lightweight |
Medical | Prosthetics, orthopedic braces, medical instruments |  | Custom-fit, biocompatible materials |
Consumer Electronics | Complex components, impact-resistant parts |  | High detail, durable |
Industrial Manufacturing | Jigs, custom tools, device casings | 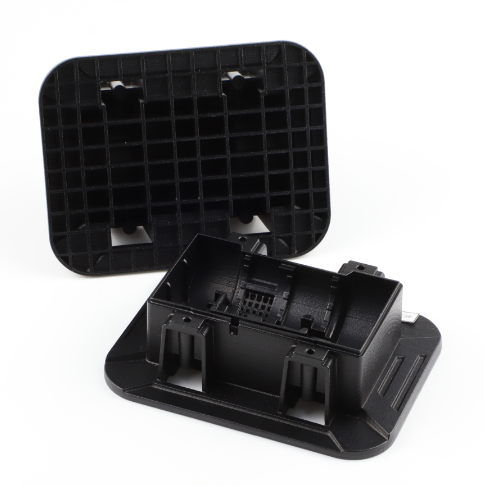 | Strong, precise, customizable |
Material Options for MJF 3D Printing
MJF uses several thermoplastic materials, each offering a different balance of performance and suitability for specific applications.
Overview of MJF 3D Printing Materials
Commonly used MJF materials include Nylon PA12, Nylon PA12 GB, Nylon PA11, polypropylene (PP), and TPU. The table below provides a quick overview of these materials, their key strengths, and typical applications.
Material | Description | Key Strengths | Typical Applications |
|---|---|---|---|
A general-purpose polyamide with a balanced combination of strength, stiffness, dimensional stability, and chemical resistance. | Balanced strength, stiffness, accuracy, and cost | Functional prototypes, housings, brackets, gears, and jigs | |
A glass-bead-reinforced PA12 grade designed for higher stiffness and dimensional stability. Its lower ductility makes it less suitable for flexible parts. | High stiffness and dimensional stability | Rigid covers, fixtures, gauges, and parts exposed to continuous loads | |
Nylon PA11 | A ductile nylon often selected for parts that require flexibility, impact resistance, or repeated movement. Some PA11 grades use renewable feedstock. | High flexibility, ductility, and impact resistance | Snap-fits, living hinges, wearables, prosthetic parts, and impact-resistant components |
Polypropylene (PP) | A lightweight material with low moisture absorption and good chemical resistance. It is often considered for fluid-related and lightweight components. | Lightweight, low moisture absorption, and good chemical resistance | Fluid containers, ducts, tanks, piping components, and lightweight parts |
A thermoplastic elastomer with rubber-like flexibility, elasticity, and wear resistance. Different TPU grades are available with different hardness levels. | Rubber-like flexibility, elasticity, and energy absorption | Seals, gaskets, vibration dampers, protective covers, and soft grips |
MJF Material Properties Comparison
MJF materials offer different combinations of strength, stiffness, flexibility, impact toughness, and heat resistance. The radar chart below provides a quick comparison of these properties across commonly used MJF materials.
The comparison evaluates materials across the following five performance dimensions:
Tensile Strength: The ability to withstand tensile loads before breaking.
Stiffness: The ability to resist deformation under load.
Flexibility: The ability to bend or deform without cracking.
Impact Resistance: The ability to absorb sudden impacts without cracking or failing.
Heat Resistance: The ability to resist deformation when exposed to heat and load.

Note: TPU scores for Impact Resistance and Heat Resistance are qualitative comparisons. The Impact Resistance score reflects TPU’s flexibility and energy-absorption capability rather than a directly comparable Izod or Charpy value.
The radar chart shows the general performance profile of each material, while the table below provides representative mechanical and thermal data.
Typical MJF Material Properties
Property | Nylon PA11 | Polypropylene (PP) | |||
|---|---|---|---|---|---|
Tensile Strength | 45–50 MPa | 29–35 MPa | 45–52 MPa | 25–32 MPa | 8–12 MPa |
Tensile Modulus | 1,600–1,800 MPa | 2,600–3,200 MPa | 1,500–1,800 MPa | 1,100–1,400 MPa | 30–100 MPa |
Elongation at Break | 15–20% | 3–10% | 35–50% | 15–30% | 150–350% |
Notched Impact Strength | 3–5 kJ/m² | 2–4 kJ/m² | 4–7 kJ/m² | 4–6 kJ/m² | No break at 23°C; 44–46 kJ/m² at −10°C |
HDT @ 0.45 MPa | 170–180°C | 170–175°C | 175–185°C | 95–110°C | Not typically reported for this grade |
HDT @ 1.82 MPa | 85–90°C | 115–125°C | 45–55°C | 50–60°C | Not typically reported for flexible TPU grades |
Part Density | 1.01 g/cm³ | 1.25–1.35 g/cm³ | 1.03–1.05 g/cm³ | 0.89–0.91 g/cm³ | 1.15–1.20 g/cm³ |
Note: The values above are for reference only and may vary depending on the material grade, printing parameters, and testing conditions.
Key Takeaways
PA12: A balanced choice for general-purpose parts and functional prototypes.
PA12 GB: Suitable when stiffness and dimensional stability are the main priorities.
PA11: Often preferred for parts that need flexibility, ductility, or impact resistance.
PP: Useful when low weight, low moisture absorption, or chemical resistance is important.
TPU: Suitable for flexible, rubber-like parts such as seals, gaskets, and vibration dampers.
MJF Post-Processing Techniques
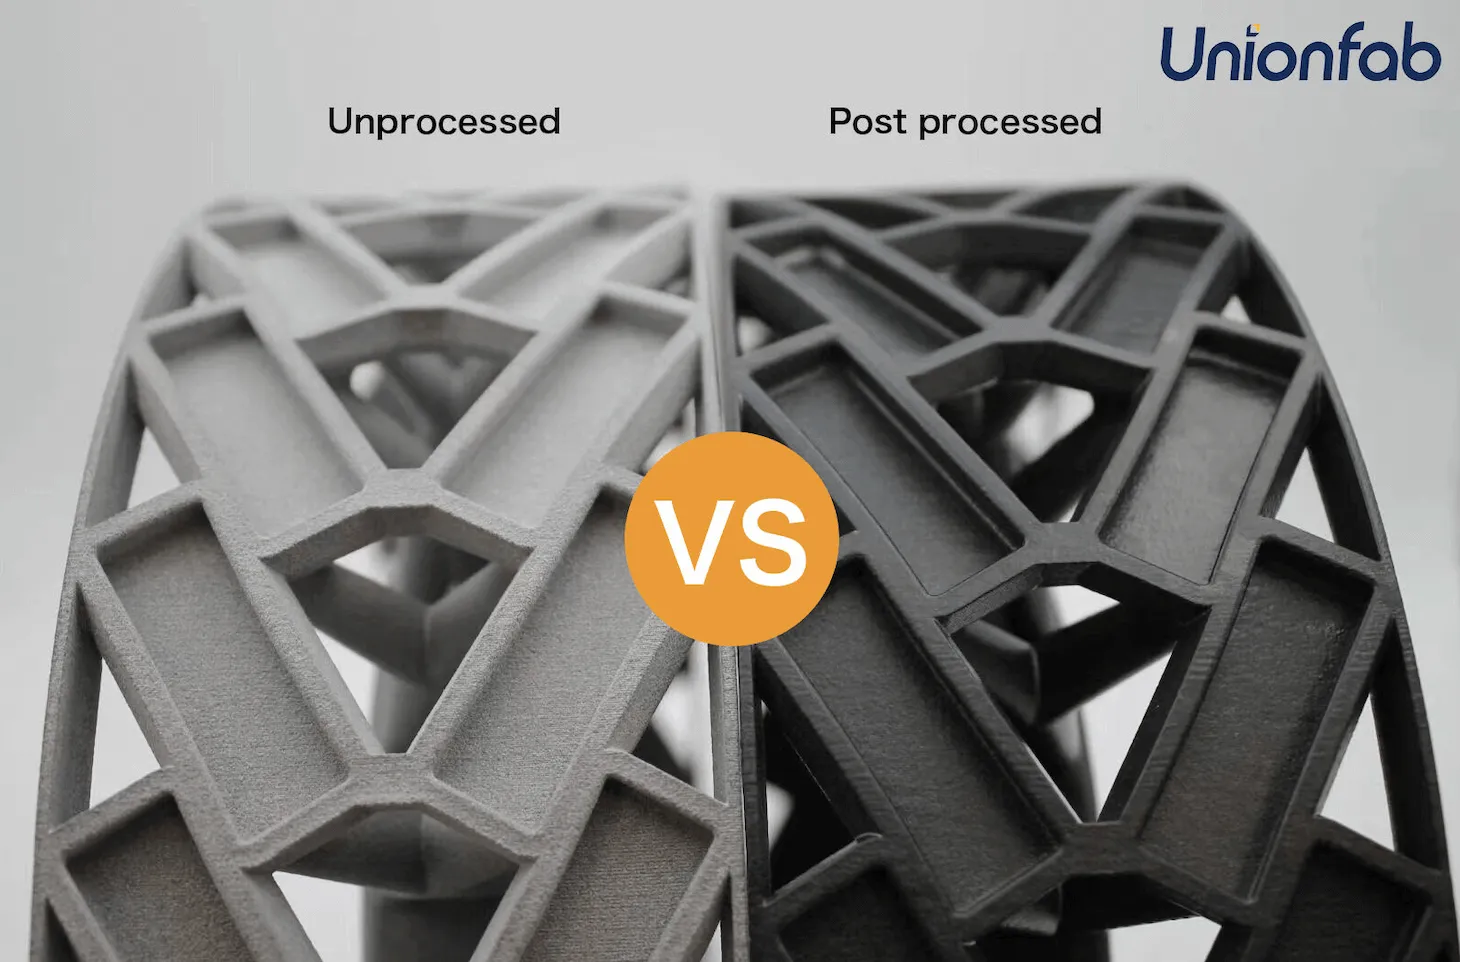
After printing, MJF parts are cooled and depowdered. Additional finishing depends on the required appearance, tolerances, and operating environment:
Depowdering and Bead Blasting: Compressed air and media blasting remove residual powder and create a uniform matte finish. The exact process depends on the part’s geometry.
Dyeing: Black dyeing is commonly used for PA12 parts. Bright or custom colors (including white) are usually achieved through painting or coating.
Vapor Smoothing: Solvent vapor softens the outer surface, reducing roughness and improving cleanability. It also seals surface porosity, though watertight or airtight performance should be validated for the specific part.
Vibratory Tumbling: Abrasive media smooths surfaces on suitable geometries, but may round sharp edges or affect tight dimensional tolerances.
Painting and Protective Coatings: Specialized coatings can add custom colors and improve wear, UV, or chemical resistance.
How Much Does MJF 3D Printing Cost?
Wondering how much MJF really costs? Here's a look at the key cost drivers—whether you're producing in-house or outsourcing to a service provider.
In-House Production Cost
Key cost factors in MJF printing include:
Machine Cost
Drawback: Industrial MJF systems like the HP Jet Fusion 5200 range from $200,000 to $400,000, depending on build size and automation features.
Advantage: Despite the high upfront investment, high throughput and material reuse help significantly reduce the long-term cost per part—especially at scale.
Material Cost
Drawback: MJF uses nylon-based powders like PA12, typically priced at $50–$80 per kilogram, which can add up quickly.
Advantage: However, the ability to reuse 70–80% of the unused powder keeps material waste and ongoing costs low, particularly in batch production environments.
Post-Processing Cost
Drawback: While some cleanup is still needed, basic post-processing like bead blasting can cost $3–$10 per part, depending on geometry and surface requirements.
Advantage: MJF parts don’t require support structures, resulting in less manual labor, shorter lead times, and smoother workflows.
ROI Analysis: Is MJF Worth the Investment?
While MJF machines come with a high upfront cost, their high production speed, minimal post-processing, and efficient powder reuse can deliver a strong return on investment (ROI), depending on production volume.
You’ll benefit most if:
You're producing 10,000+ parts per year
You need rapid iteration without supplier delays
You want tight control over design and production workflows
When to Use a 3D Printing Service Instead?
Outsourcing to a service provider like Unionfab can be smarter in many scenarios:
In-House Production | Outsourcing (Via Service Provider) |
|---|---|
✔ High print volume (>10,000 parts/year) | ✔ Low to mid volume (<5,000 parts/year) |
✔ Need for fast internal turnaround | ✔ Occasional or on-demand printing |
✔ Full control over design iterations | ✔ Access to wide material/finish options |
❌ High initial capex & maintenance | ✔ Zero upfront investment |
❌ Limited material inventory | ✔ One-stop access to the latest technologies |
Get real-time pricing for your MJF parts—use our Cost Calculator to see your estimated cost instantly.
Design Tips for MJF 3D Printing
MJF can produce strong and complex parts without traditional support structures. However, good design practices help reduce warping, trapped powder, and parts fusing together.
The values below are general guidelines. Actual limits may vary depending on the material, printer, part geometry, and service provider.
Wall Thickness: A minimum of about 0.7–0.8 mm is often used, while 1.5–3 mm is a safer range for general parts. Keep wall thickness as consistent as possible. For thick solid areas, consider hollowing the part or adding ribs.
Moving Parts: Leave around 0.5–0.7 mm of clearance between moving or interlocking surfaces. Tighter clearances may be possible, but should be confirmed with the manufacturer.
Hollow Parts: Add at least two powder-escape holes. Use larger holes for large or deep cavities so that the unused powder can be removed more easily.
Holes and Channels: Holes of around 2 mm or larger are a practical starting point. Deep, narrow, or blind holes may need larger openings or additional cleaning.
Large Flat or Long Features: Large flat surfaces and long, thin sections are more likely to warp. Add ribs, chamfers, cutouts, or curved surfaces where possible. An aspect ratio above roughly 10:1 should be treated as a warning sign, not a strict limit.
Embossed and Engraved Details: Use a line width and feature height/depth of about 0.5 mm or more. For readable text, a character height of approximately 2.5 mm or larger is a safer choice, especially after bead blasting or dyeing.
Snap-Fits and Flexible Parts: Add fillets at the roots of snap-fit arms and avoid sharp corners. PA11 is often a good choice for parts that need repeated flexing, when available.
Threads and Fasteners: Use threaded inserts for repeated assembly or higher loads. Printed threads can work for larger sizes and light-duty applications, but the recommended size should be confirmed with the service provider.
MJF vs. SLS vs. SLA vs. FDM: Which Is Right for Your Project?
Different 3D printing technologies suit different project requirements. The best choice depends on factors such as part geometry, material requirements, production volume, surface finish, and budget.
How It Works | Inkjet-deposited fusing and detailing agents combined with infrared energy | Laser selectively sinters polymer powder | UV light cures liquid photopolymer resin | Melts and extrudes thermoplastic filament layer by layer |
Speed | Fast for many nested parts and batch production | Moderate; point-by-point laser scanning can take longer for dense builds | Varies by printer, layer height, and part size | Varies by printer, material, and part geometry |
Materials | PA12, PA11, PP, and TPU on compatible systems | Nylon, TPU, PP, and composite powders, depending on the system | Standard, tough, high-temperature, and elastomeric resins | PLA, ABS, PETG, nylon, PC, TPU, and carbon-fiber-filled filaments |
Part Strength | High; relatively consistent mechanical properties across directions | High; suitable for many functional polymer parts | Depends on the resin; some grades are brittle, while others are designed for toughness | Directional; strength is often lower between layers than within a layer |
Surface Finish | Uniform matte or slightly grainy finish; can be dyed or vapor smoothed | Matte, slightly grainy finish; can be bead blasted or dyed | Smooth finish with fine details; support removal and UV curing are usually required | Visible layer lines; sanding, smoothing, or coating may improve the finish |
Best For | Functional prototypes, complex assemblies, and low- to medium-volume production | Functional prototypes, complex nylon parts, and small-batch production | High-detail models, visual prototypes, patterns, and selected engineering applications | Low-cost prototypes, large concept parts, fixtures, and tooling |
Relative Cost | $$ | $$ – $$$ | $ – $$$ | $ |
Key Takeaways
MJF provides the best balance of speed, isotropic strength, and batch efficiency, making it the top choice for functional end-use polymer parts.
SLS is the proven industrial standard for complex, support-free nylon components and functional prototypes requiring maximum material diversity.
SLA delivers unparalleled resolution and smooth surface quality. While standard resin is best for aesthetics, modern engineering resins make functional validation possible.
FDM remains the most accessible and budget-friendly option for concept models and custom tooling, though layer orientation directly impacts mechanical performance.
If you're unsure which process fits your project best, our engineering team is ready to help you optimize and quote your design.
Unionfab's MJF 3D Printing Services
With 20+ years of manufacturing experience, Unionfab provides industrial MJF 3D printing with scalable production capacity, fast lead times, and comprehensive quality control.
MJF Materials Available
Unionfab offers a range of MJF materials to meet different functional, mechanical, and application requirements, including:
Nylon 12 (Raw Grey) – A versatile material for functional prototypes and end-use parts, offering a good balance of strength, durability, and dimensional stability.
Nylon 12 Glass Bead – Glass bead-filled nylon with increased stiffness and dimensional stability for applications requiring greater rigidity.
HP 3D HR PA 12 FR – A flame-retardant PA 12 material designed for applications where improved fire resistance is required.
Ultrasint TPU01 – A flexible TPU material suitable for parts requiring elasticity, impact resistance, and rubber-like properties.
Scalable In-House MJF Production
10× HP MJF 4200 printers
8× HP MJF 5200 printers
6 production facilities across China
Fast, Accurate, and Reliable
3-day standard lead time
CMM inspection for critical dimensions and tolerances
Full batch traceability and quality documentation
Hassle-Free Ordering, Support & After-Sales
Real-time quoting and order tracking
24/7 online support
Advanced Finishing Options at Unionfab
In addition to standard post-processing, Unionfab offers a wide range of professional finishing and surface treatment options to meet different aesthetic, functional, and application requirements:
Painting & Surface Finishes: Regular Spray Paint, Crackle Paint, Matte Finish, Glossy Finish
Plating & Coating: Nickel Plating, Tin Plating, Zinc Plating, Electroplating, Electrolytic Plating, Vacuum Plating
Etching & Engraving: Laser Engraving, Texture Etching, Mold Etching
Printing & Decoration: Silk Screen Printing, Pad Printing, Water Transfer Printing, Heat Transfer Printing, Hot Stamping, UV Printing
Surface Preparation: Sandblasting
Whether you want your parts to achieve a premium appearance, withstand demanding environments, or meet specific application requirements, Unionfab's finishing capabilities provide a wide range of options.
Haven't used Unionfab's 3D printing services yet? Sign up now and get 10% off your first order.
Customer Feedback
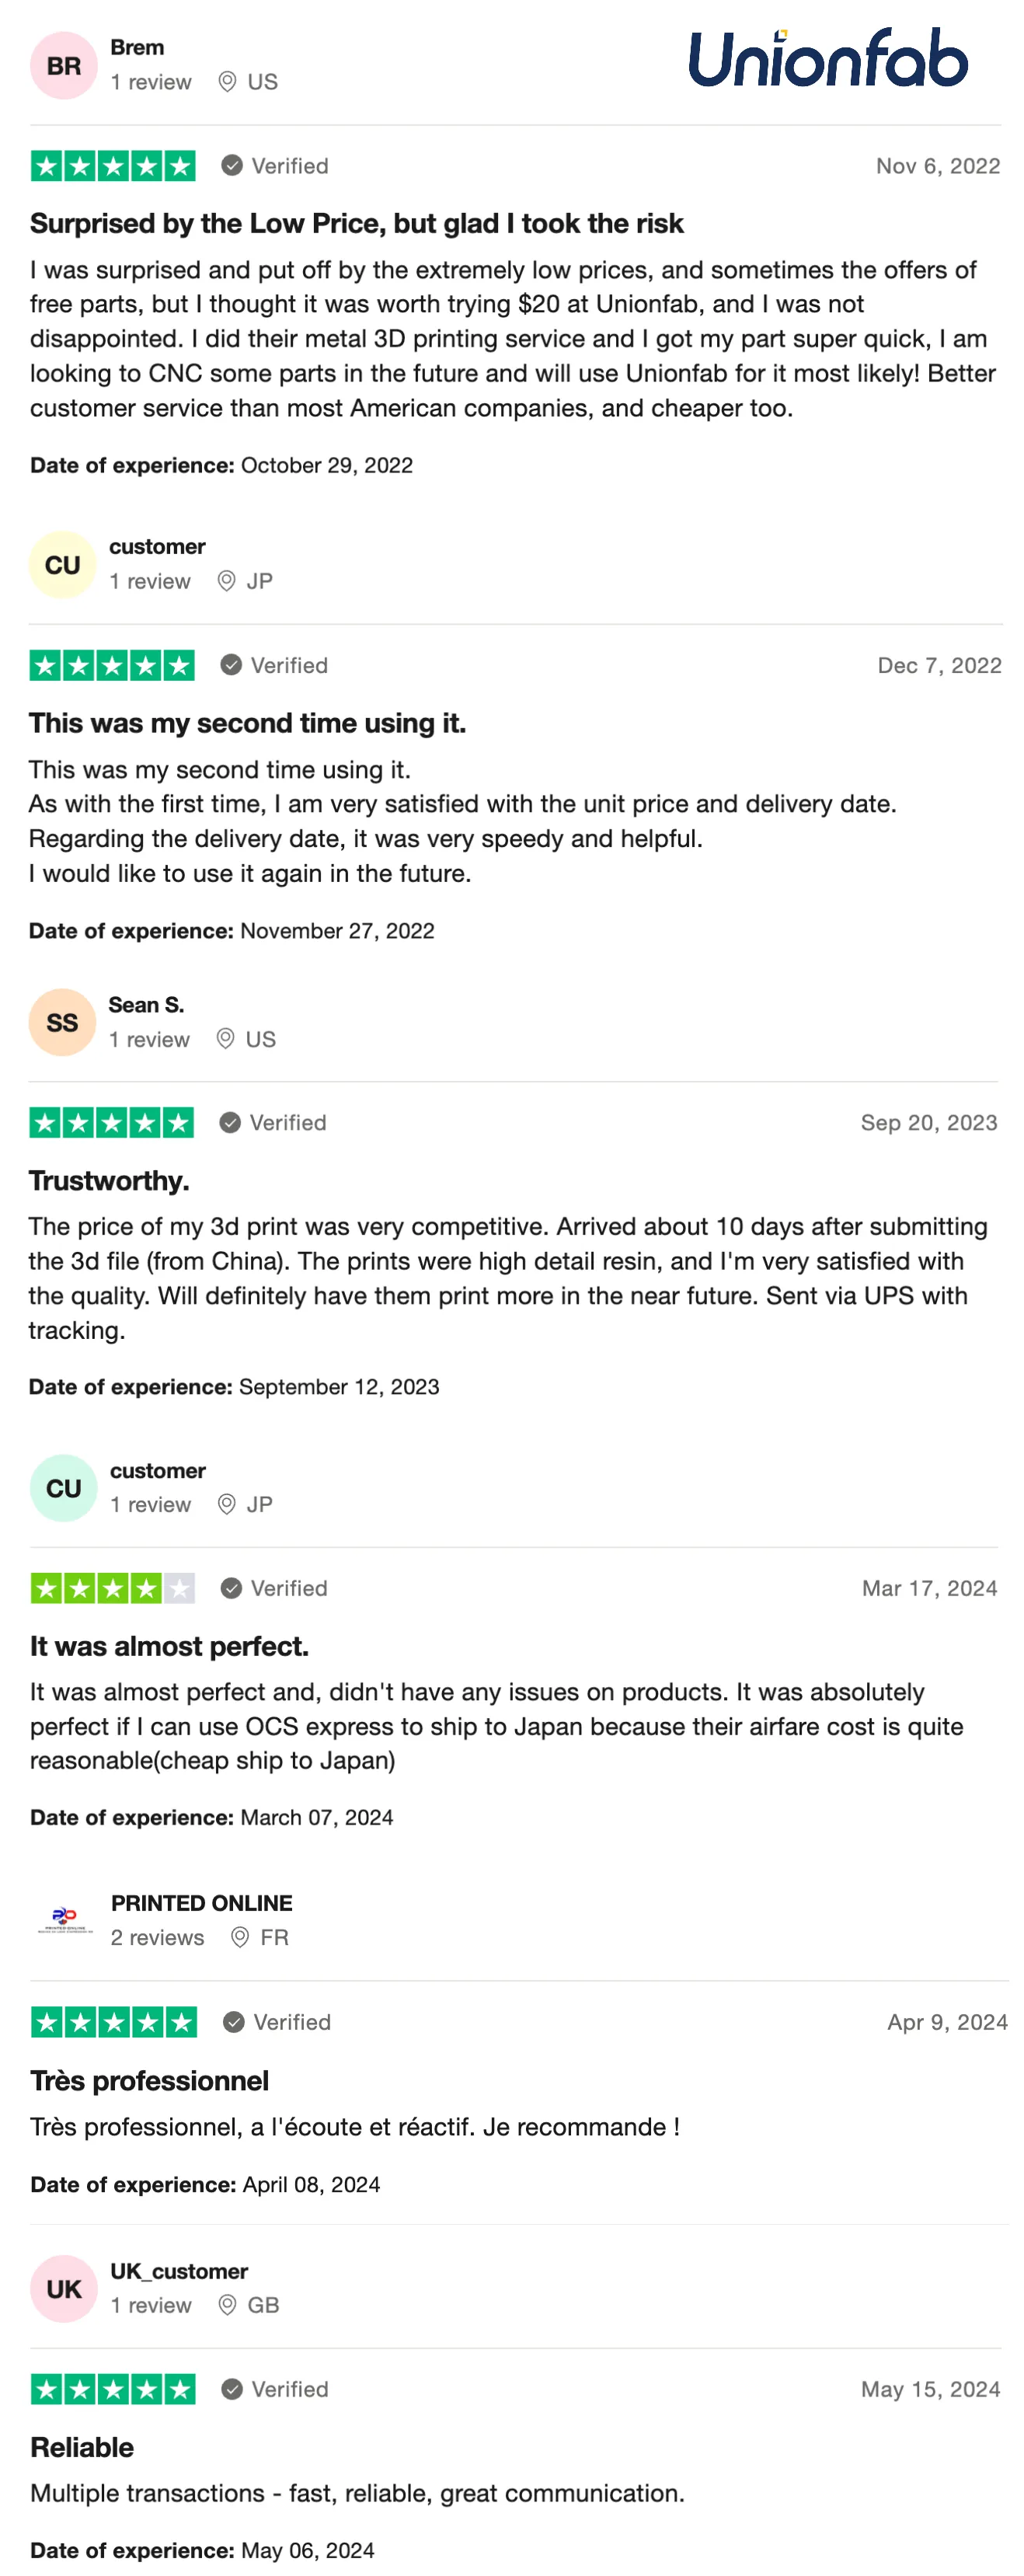
Here’s what customers are saying about Unionfab on Trustpilot:
Customer | Feedback |
|---|---|
Brem from US | ★★★★★ Surprised by the Low Price, but glad I took the risk. I was surprised and put off by the extremely low prices, and sometimes the offers of free parts, but I thought it was worth trying $20 at Unionfab, and I was not disappointed. I did their metal 3D printing service and I got my part super quick, I am looking to CNC some parts in the future and will use Unionfab for it most likely! Better customer service than most American companies, and cheaper too. |
Customer from JP | ★★★★★ This was my second time using it. As with the first time, I am very satisfied with the unit price and delivery date. Regarding the delivery date, it was very speedy and helpful. I would like to use it again in the future. |
Sean. S from US | ★★★★★ Trustworthy. The price of my 3D print was very competitive. Arrived about 10 days after submitting the 3D file (from China). The prints were high detail resin, and I'm very satisfied with the quality. Will definitely have them print more in the near future. Sent via UPS with tracking. |
Customer from JP | ★★★★ It was almost perfect. It was almost perfect and didn't have any issues on products. It was absolutely perfect if I can use OCS express to ship to Japan because their airfare cost is quite reasonable (cheap ship to Japan). |
Printed Online from FR | ★★★★★ Très professionnel Très professionnel, à l'écoute et réactif. Je recommande! |
UK_customer from GB | ★★★★★ Reliable. Multiple transactions - fast, reliable, great communication. |
FAQs About MJF 3D Printing
Can MJF parts be used outdoors?
Yes. PA12 offers good resistance to moisture and abrasion, making MJF parts suitable for many outdoor applications. For prolonged exposure to sunlight, UV-resistant coatings or other protective finishes can help improve weathering resistance.
What’s the minimum order volume for MJF parts?
At Unionfab, there is no minimum order quantity (MOQ). Whether you need a single prototype or 10,000+ parts, we can accommodate different production volumes.
Is MJF waterproof?
MJF PA12 parts are not inherently watertight in their as-printed state. Depending on the part geometry and application, fluids may permeate through small pores or pathways. Sealing, coating, or other post-processing methods can improve water resistance and help achieve watertight performance for suitable applications.
So, MJF parts can be made suitable for waterproof or watertight applications with the right post-processing, but they are not guaranteed to be watertight as printed.
Does MJF printing need supports?
No. One of the major advantages of MJF is that it doesn’t require support structures. The surrounding powder supports the part during printing, allowing greater design freedom, reducing material waste, and helping shorten turnaround times.
What are the advantages of MJF?
MJF offers good detail, dimensional accuracy, and repeatability, along with excellent mechanical strength, particularly with PA12. It also produces a consistent matte surface finish and does not require support structures. These advantages make MJF suitable for both functional prototypes and end-use parts, as well as low- to mid-volume production.
What are the disadvantages of MJF?
MJF has a more limited material selection than some other 3D printing methods. As-printed parts typically have a matte, slightly grainy surface finish, and additional sealing or post-processing may be required for watertight or airtight applications. For in-house production, the relatively high initial equipment cost can also be a consideration.